Discover the latest industry trends, formulation R&D innovations, and Italian cosmetics manufacturing expertise from our team of specialists.
Explore our premier line of high-performance airless pump containers, custom formulations, and turnkey beauty sets engineered to safeguard sensitive active ingredients from oxidation while delivering exceptional shelf appeal.
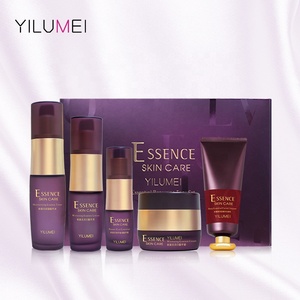
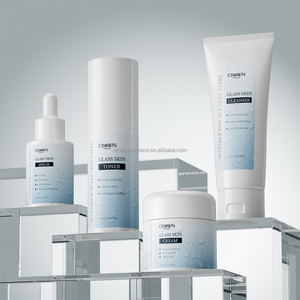
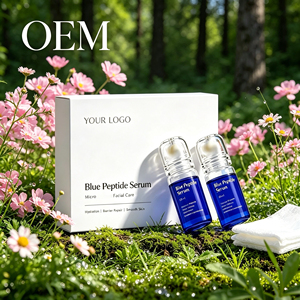
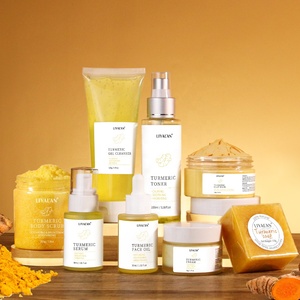
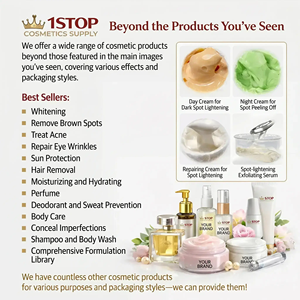
In the contemporary cosmetic manufacturing sector, packaging is no longer a passive vessel; it is an active mechanical delivery system. Airless pump technology represents the pinnacle of protective cosmetic packaging, specifically designed to mitigate oxidation, prevent microbial ingress, and optimize active ingredient bio-availability.
Unlike traditional dip-tube systems relying on atmospheric displacement, our airless containers utilize a precision-molded internal piston mechanism. Upon actutation, a micro-vacuum is generated within the chamber, drawing the piston upward and delivering a consistent dosage without exposing remaining formulation to ambient air.
Formulations enriched with L-Ascorbic Acid (Vitamin C), Retinoids, Copper Peptides, and natural botanical extracts undergo rapid hydrolytic and oxidative degradation when exposed to oxygen. Our non-return valve engine maintains headspace oxygen concentration below 0.05%, preserving formulation potency throughout the product lifecycle.
Consumer dissatisfaction often stems from standard dip-tube bottles leaving up to 15% of product trapped at the base. Our engineered airless pump containers achieve up to 98.5% evacuation rates, maximizing consumer value and minimizing formula wastage.
Achieving optimal dosage delivery requires precise technical pairing between formulation viscosity (measured in Centipoise, cP) and pump engine orifice architecture. The following engineering matrix details standard parameters utilized across our state-of-the-art manufacturing facilities.
| Formulation Category | Viscosity Range (cP) | Recommended Airless System | Dosage Output (ml) | Primary Material Options |
|---|---|---|---|---|
| Hydrating Serums & Essences | 1,000 – 5,000 cP | Single Valve Micro-Engine Piston | 0.15 ml / 0.20 ml | PETG / Glass / PCR-PP |
| Active Emulsions & Lotions | 5,000 – 25,000 cP | Dual-Valve Spring-External Engine | 0.25 ml / 0.50 ml | PP / AS / High-Barrier Acrylic |
| Barrier Creams & Heavy Pastes | 25,000 – 90,000 cP | High-Pressure Airless Jar / Soft Touch Pouch | 0.50 ml / 1.00 ml | Mono-material Polyolefin (PP) |
| Sensitive Multi-Phase Actives | Variable (10,000 – 40,000 cP) | Dual-Chamber Separated Airless Bottle | 0.20 ml + 0.20 ml Dual Dosage | Acrylic Outer / Polypropylene Inner |
As brand owners, procurement managers, and contract manufacturers navigate tighter environmental regulations and shifting consumer preferences, purchasing strategies for airless packaging are undergoing significant structural transformations.
Historically, airless pump engines relied on internal metal springs and multi-resin elastomer valves, rendering them difficult to process in standard municipal recycling streams. The modern procurement imperative centers on Mono-material Polypropylene (PP) packaging. By utilizing all-PP pump engines—including plastic-spring technology—brands can market fully recyclable finished goods (Class 5 PP stream) that comply with stringent European Union packaging waste directives.
Global beauty conglomerates are enforcing strict corporate sustainability mandates requiring 30% to 100% PCR resin content by 2026. China’s advanced injection molding infrastructure now enables high-precision PCR-PP and PCR-PETG airless bottle manufacturing without compromising structural integrity, dimensional tolerances, or aesthetic clarity.
Luxury skincare brands are rapidly adopting eco-refill airless architectures. These modular systems feature a durable, high-end outer shell (such as thick-walled glass or polished acrylic) combined with a replaceable internal airless cartridge. Procurement costs for brand replenishments are reduced by up to 40% per refill unit, simultaneously reducing plastic mass consumption by over 70%.
Strategic beauty buyers are moving away from fragmented sourcing models where bottles are purchased from one vendor and bulk liquid is manufactured by another. Sourcing directly from an integrated manufacturer—combining cleanroom filling, formulation development, and container tooling—eliminates container-formula incompatibility risks such as pump clogging, seal swelling, or dosage leakage.
As a leading Chinese manufacturer and global exporter of high-precision cosmetic packaging and formulations, our facilities bridge Italian cosmetic craftsmanship with China’s industrial scale and efficiency. Operating across fully automated Class 100,000 cleanrooms, our factory delivers flawless execution from initial 3D rapid prototyping to high-speed bulk filling.
Our comprehensive quality control protocol includes automated vision inspection systems, 100% inline micro-vacuum leak testing, and stringent raw material assay validations. Whether you require standard wholesale airless bottles or custom formulation OEM services, we guarantee compliance with global international cosmetic regulations.
Strict adherence to Good Manufacturing Practices ensuring zero contamination throughout assembly and filling operations.
Certified Quality Management Systems guaranteeing batch-to-batch dimensional accuracy and dosage precision.
Environmental management protocols focused on energy reduction, zero land consumption, and waste recycling.
Full compliance options for cruelty-free, vegan, and Halal certified skincare formulations and production lines.
Everything you need to know about airless pump container wholesale, custom mold development, formulation testing, and global exporting procedures.